What Is OEE? How to Calculate It, What a Good Score Is, and How to Track It in Real Time with IoT
SMART FACTORY · MACHINE MONITORING
What Is OEE?
The One Number That Tells the Truth About Your Machines
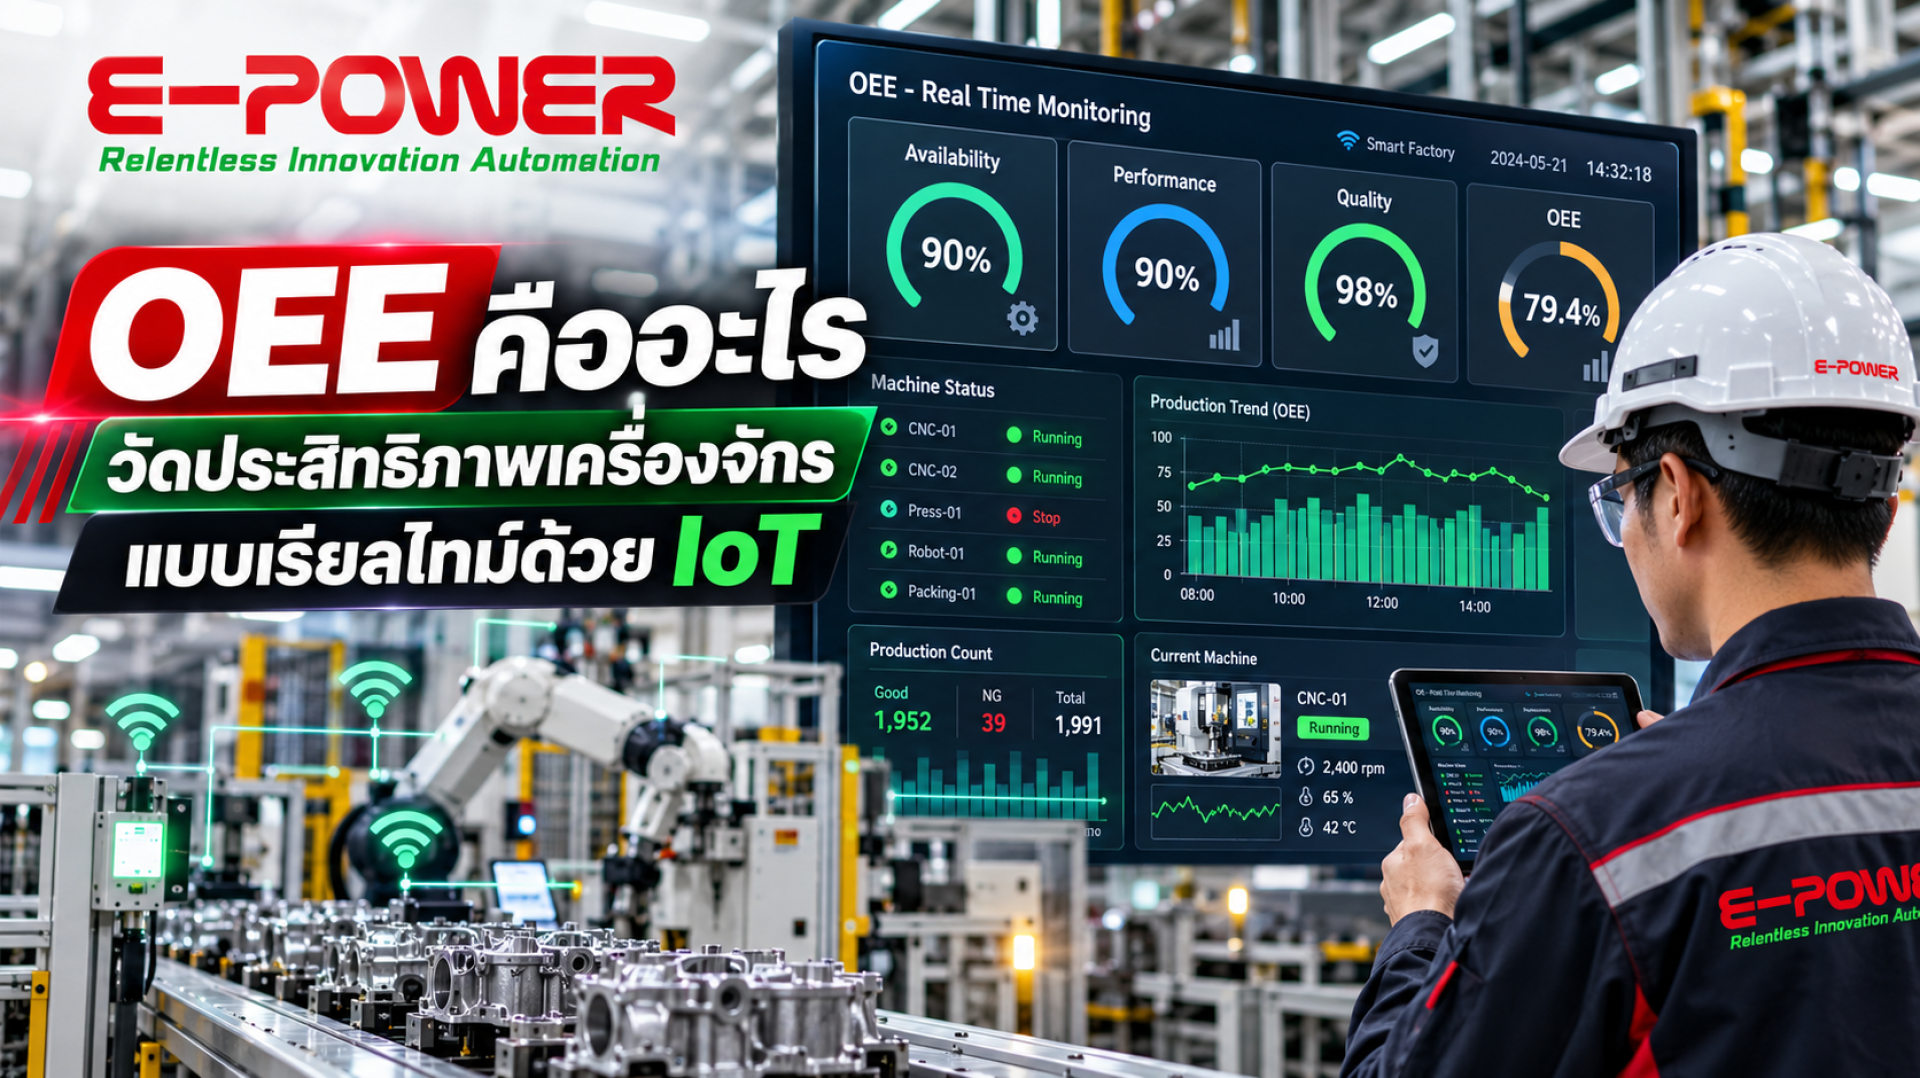
Machines run all day, yet output misses target? OEE shows exactly where the time goes, and IoT lets you see it during the shift.
What is OEE?
OEE measures what percentage of a machine's full potential, during planned time, is turned into good parts. The concept comes from Japan, developed by Seiichi Nakajima as the core metric of TPM (Total Productive Maintenance), and it has become a standard KPI in manufacturing worldwide.
If a machine runs every planned minute, at full speed, with zero defects, OEE = 100%. Every missing percentage point is a loss you can fix.
The OEE formula
A · Availability
Run time ÷ Planned production time
Captures losses from stops such as breakdowns, changeovers, setups, and waiting for material
P · Performance
(Ideal cycle time × Total count) ÷ Run time
Captures losses from running slower than standard or frequent small stops
Q · Quality
Good count ÷ Total count
Captures losses from scrap, rework, and parts made during startup
Ideal cycle time = the theoretical fastest time to produce one part, from the machine specification or the best rate ever achieved.
Example: where does an 8-hour shift go?
Scenario: 30-minute break, 45 minutes of breakdowns and changeovers, ideal cycle time 1.5 seconds per part, 14,580 parts produced, 14,288 of them good.
The 480-minute shift timeline
Each factor looks strong at 90% or more, yet multiplied together they fall below 80%. The timeline shows that only about 357 of 480 minutes produced good parts at full speed. That is why OEE never lets small losses hide.
What is a good OEE?
The 85% world-class benchmark comes from roughly 90% Availability, 95% Performance, and 99.9% Quality. The right target also depends on the type of production: continuous processes usually reach higher OEE than lines with frequent changeovers. More important than any target is steady improvement over time.
The Six Big Losses that drag OEE down
AVAILABILITY LOSS
Breakdowns: burned-out motors, electrical faults
Setups and changeovers: mold changes, adjustments
PERFORMANCE LOSS
Small stops: jams, blocked sensors
Reduced speed: running slow due to wear
QUALITY LOSS
Startup rejects: first parts after a changeover
Production rejects: wrong size, defects, rework
The invisible culprit: loss , small stops. Each lasts only seconds, so nobody records it, yet across a shift they can add up to tens of minutes. An IoT system that logs machine status automatically catches every one.
Paper logs vs real-time OEE with IoT
| Paper / Excel | Real-time IoT | |
| When you see results | After the shift or day ends | During the shift, fix it now |
| Small stops | Almost all missed | Logged to the second |
| Reliability | Depends on who records, rounding, forgetting | Straight from the machine, unbiased |
| Comparison | Hard and time-consuming | Every machine, shift, and line on one screen |
How do you collect OEE data, even from old machines?
The system needs only four data points, and they can be collected from new machines with PLCs and from older machines with no digital controls at all, without modifying the original equipment.
Run / stop status
With PLC: read via Modbus · Older machine: CT on motor current or a contactor signal
Total count
With PLC: read the counter · Older machine: proximity or photoelectric sensor counting parts
Reject count
With PLC: inspection system signal · Older machine: sensor on the reject chute or a button at the machine
Stop reasons
With PLC: alarm codes · Older machine: reason buttons on an HMI or tablet
Real-time OEE with the E-POWER IoT Platform
️ 4 common mistakes when starting with OEE
Setting ideal cycle time too slow Performance looks inflated and problems stay hidden
Counting unplanned stops as breaks Availability looks better than it is
Looking only at the overall OEE you can't tell which factor to fix
Using OEE to blame operators data gets distorted instead of revealing root causes
Frequently asked questions about OEE
Q. What is OEE?
A measure of overall equipment effectiveness: the percentage of a machine's full potential, during planned time, that becomes good output.
Q. How is OEE calculated?
OEE = Availability × Performance × Quality: actual run time vs plan, times actual speed vs standard, times the share of good parts.
Q. What is a good OEE score?
World class is about 85% or higher, typical plants are around 60%, and below 40% needs urgent improvement.
Q. Can older machines without a PLC be measured?
Yes. A CT on the motor current shows run/stop status and a sensor counts parts, both feeding an IoT gateway without modifying the machine.
Q. How are OEE and TPM related?
OEE is the key metric of TPM, used to track progress in reducing all six types of equipment loss.
Want to see your machines' OEE in real time?
E-POWER engineers deliver complete machine data systems, from sensor installation and PLC connection to OEE dashboards and alerts, for both new and older machines.
Talk to us on LINE @epower info@epower.co.thTel. +66 81-559-5145 | YouTube: Epower Service | TikTok: epowerservice_
Read next: What is a CT and why use it with a power meter · Complete guide to industrial sensors · Modbus RTU vs Modbus TCP · What is an industrial edge AI computer · CODESYS Runtime